Z Purlin Roll Forming Machine: Guide, Specs & Models
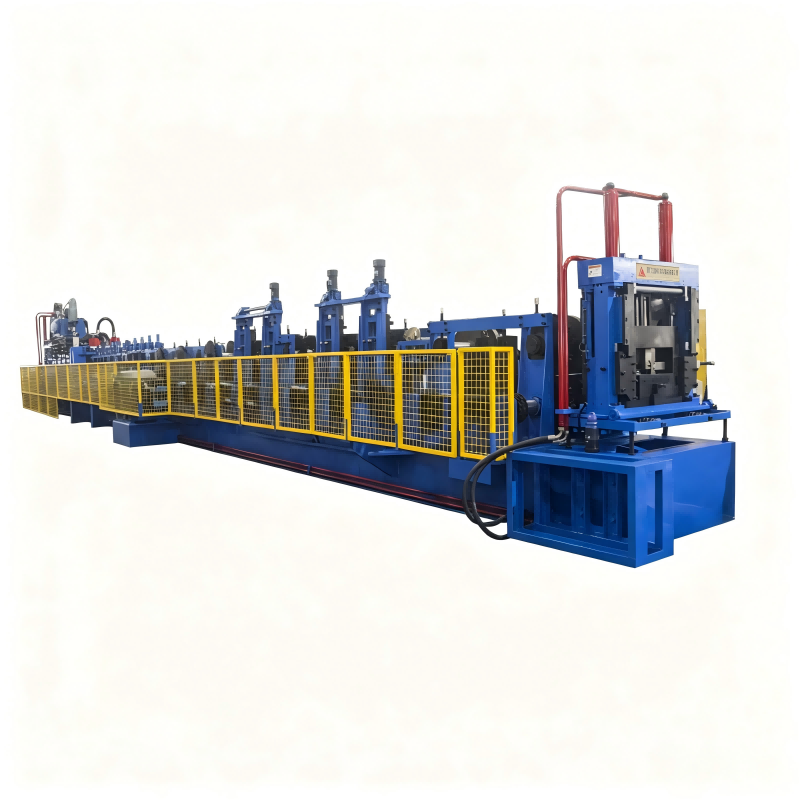
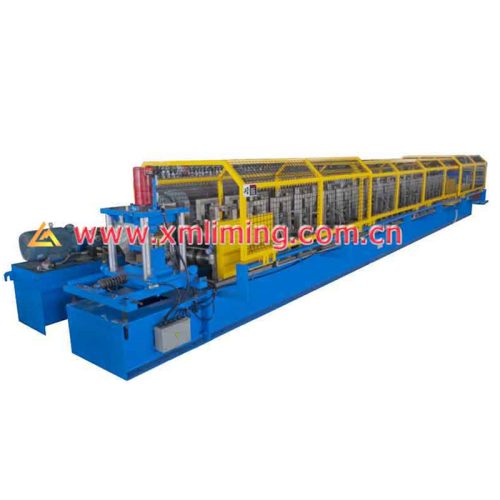
A Z purlin roll forming machine is a dedicated cold roll forming production line that shapes flat steel coils into Z-shaped structural purlins. As a specialized type of purlin roll forming machine, Z-profile lines are engineered for long-span roof systems, where overlapping flange design enables continuous load transfer across multiple building bays.
For steel fabricators, prefab builders and construction material suppliers, a reliable Z purlin machine directly impacts production efficiency, profile accuracy and on-site installation fit. This guide covers everything you need to evaluate before sourcing a purlin roll forming machine for Z-section production: working principle, automatic models, frame options, core components, key benefits, selection criteria and FAQs.
You can also check our purlin machine product page for detailed configuration options and factory pricing.
What Is a Z Purlin Roll Forming Machine?
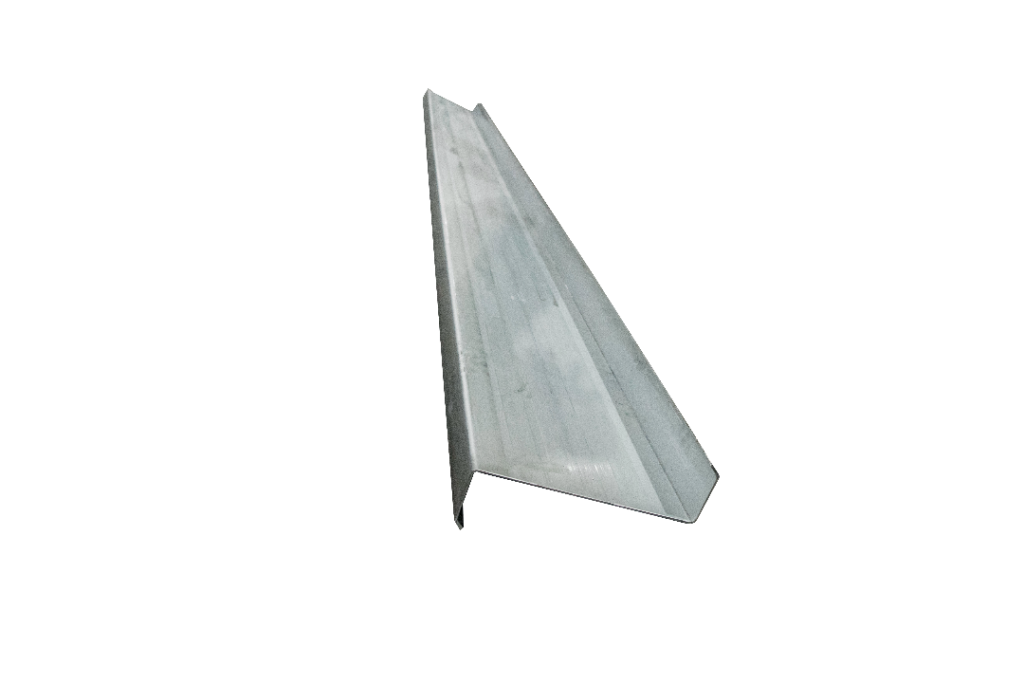
A Z purlin roll forming machine is a continuous cold-bending purlin making machine that produces Z-shaped steel purlins from coiled raw material. Unlike symmetrical C-shaped profiles, Z purlins feature offset overlapping flanges that allow nested splicing, making them the preferred framing component for large-span industrial warehouses, factories and commercial steel buildings.
If you also produce C profiles, see our C purlin roll forming machine guide for a full comparison.
A finished Z purlin typically includes:
A vertical web plate
Two offset horizontal flanges (opposite-direction Z geometry)
Stiffened lips for enhanced load-bearing capacity
Pre-punched mounting holes for fast on-site assembly
Standard Z purlin forming machine configurations are available as automatic adjustable systems. In industrial sourcing, many buyers also refer to this equipment simply as a Z purlin machine.
What Does a Z Purlin Making Machine Produce?
A Z purlin making machine manufactures Z-shaped steel sections used across a wide range of structural applications:
Main roof purlins for large-span industrial and commercial buildings
Secondary framing for warehouses, workshops and exhibition centers
Support members for agricultural steel structures and grain silos
Wall girts for heavy-duty exterior cladding systems
Prefabricated steel building component manufacturing
For solar mounting profiles, see our solar mounting roll forming machine.
Compatible materials include cold-rolled steel coil and galvanized steel coil with yield strength of 235 MPa or 345 MPa. Standard processing thickness ranges from 1.5 mm to 3.0 mm depending on the machine model.
Note: The purlin machine is the production equipment; the Z purlin is the finished profile. When sourcing equipment for high-volume production, confirming your profile drawing and material thickness first will help you get the most accurate quotation.
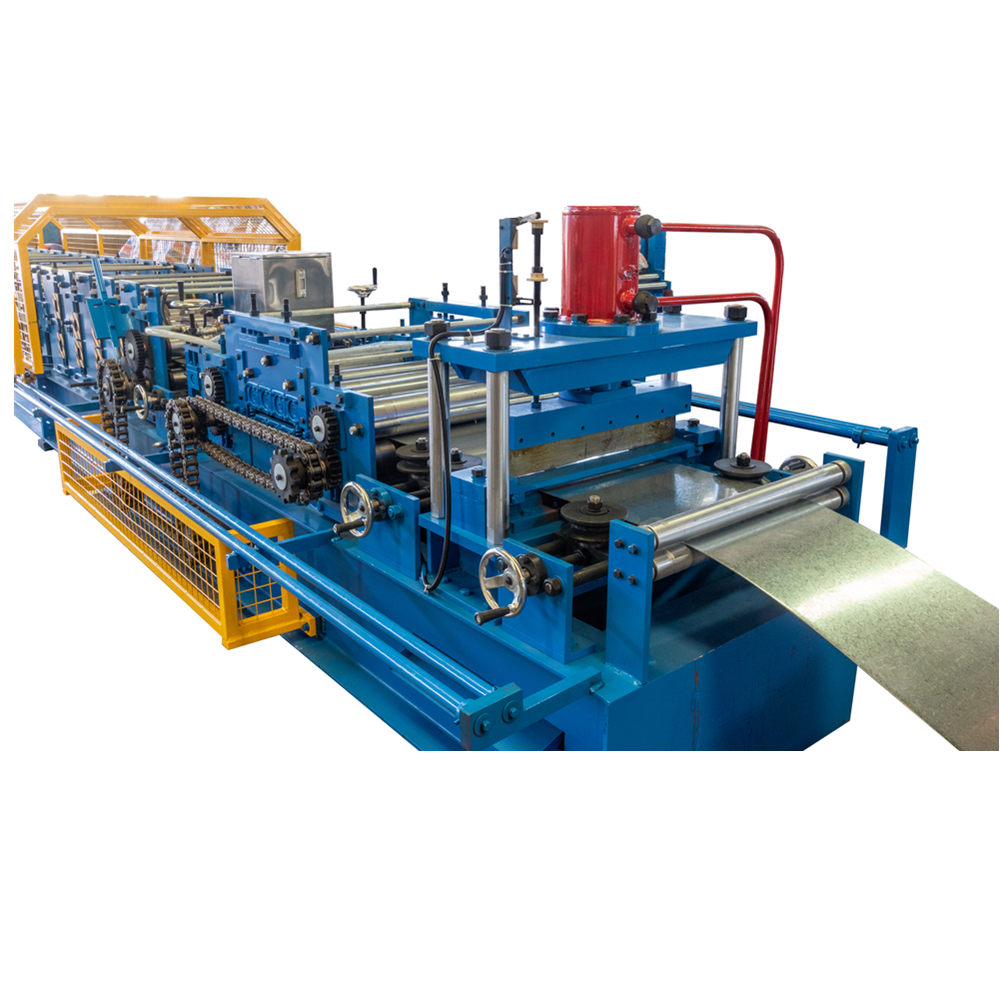
How Does a Z Purlin Roll Forming Machine Work?
Standard Z purlin lines use a pre-punching and post-cutting workflow for maximum profile accuracy and clean edge finish. The process follows six sequential core stages:
1. Coil Decoiling
The raw steel coil is loaded onto a decoiler and unwound at controlled tension to feed the forming line steadily. Manual cantilever decoilers and hydraulic expansion decoilers are available to match different automation levels.
2. Pre-Leveling & Guided Feeding
The strip passes through a 7-roller leveling unit (4-over-3 arrangement, Φ95 mm leveling rollers) to remove coil set and surface bow, then enters the processing section with precise edge alignment.
3. Hydraulic Pre-Punching
Before forming, hydraulic punching stations punch mounting holes into the flat strip at pre-set intervals. Standard hole configurations include:
Bottom double holes – Punching Unit 1: 14×22 mm
Bottom single hole – Punching Unit 2: 14×22 mm
Side flange double holes – Punching Unit 3: 14×22 mm
Punch cylinder bore: Φ110 mm
This ensures accurate hole positioning and avoids profile deformation after forming.
4. Progressive Roll Forming
The strip travels through paired forming stations. Each station bends the material a small increment until the full Z cross-section is achieved. Gradual forming ensures uniform stress distribution and accurate flange geometry.
5. Hydraulic Post-Cutting
After full profile forming, a universal hydraulic shear with Cr12MoV heat-treated blades cuts the Z purlin to the target length. Cutting tolerance is ±1 mm. A slug breaker is included for high-volume production.
6. Finished Product Output
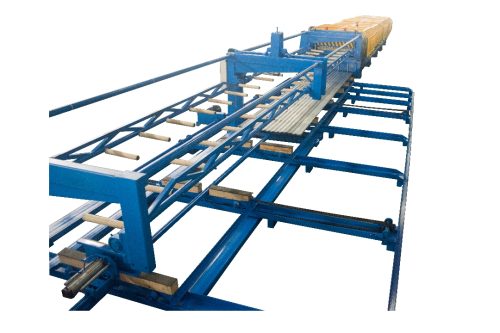
Cut Z purlins exit onto a 6-meter unpowered run-out rack (3 m × 2 sections) for collection, packaging and transport.
This continuous workflow is why a Z purlin forming machine delivers much higher output and dimensional consistency than manual press-brake forming methods.
Automatic Z Purlin Machine Models & Specifications
Our automatic Z purlin roll forming machines are available in three configurations: Z100-300 (archway-type) , Z100-300 (pillar-type) and Z100-350.
Z100-300 (Archway-Type)
| Parameter | Specification |
| Model | Z100-300 (135°) |
| Web Height | 45–80 mm |
| Material | Cold-rolled steel, galvanized steel |
| Thickness | 1.5–3.0 mm |
| Yield Strength | 235 MPa / 345 MPa |
| Forming Stations | 15 (forming) + 1 (up/down bending) + 1 (side bending) |
| Roller Material | Cr12, precision machined, heat-treated, polished |
| Shaft | Φ75 mm, 45# steel, precision machined |
| Frame | 450H |
| Side Plate | Archway type, 38 mm |
| Main Drive Motor | 30 kW (Inovance servo motor) |
| Production Speed | 30 m/min |
| Transmission | Gear / sprocket drive, 1.5-inch chain |
| Cutting Tolerance | ±1 mm |
| Machine Dimensions | 11,200 × 1,850 × 1,860 mm |
| Machine Weight | Approx. 15 T |
Z100-300 (Pillar-Type)
| Parameter | Specification |
| Model | Z100-300 (135°) |
| Web Height | 45–80 mm |
| Material | Cold-rolled steel, galvanized steel |
| Thickness | 1.5–3.0 mm |
| Yield Strength | 235 MPa / 345 MPa |
| Forming Stations | 16 (forming) + 1 (up/down bending) + 1 (side bending) |
| Roller Material | Cr12, precision machined, heat-treated, polished |
| Shaft | Φ75 mm, 45# steel, precision machined |
| Frame | 450H |
| Side Plate | Pillar type, 59×59 mm |
| Main Drive Motor | 30 kW (Inovance servo motor) |
| Production Speed | 30 m/min |
| Transmission | Gear / sprocket drive, 1.5-inch chain |
| Cutting Tolerance | ±1 mm |
| Machine Dimensions | 12,300 × 1,800 × 2,000 mm |
| Machine Weight | Approx. 17.4 T |
Z100-350
| Parameter | Specification |
| Model | Z100-350 (135°) |
| Web Height | 45–100 mm |
| Material | Cold-rolled steel, galvanized steel |
| Thickness | 1.5–3.0 mm |
| Yield Strength | 235 MPa / 345 MPa |
| Forming Stations | 16 (forming) + 1 (up/down bending) + 1 (side bending) |
| Roller Material | Cr12, heat-treated, polished |
| Shaft | Φ75 mm, 45# steel, precision machined |
| Frame | 450H |
| Side Plate | Pillar type, 59×59 mm |
| Main Drive Motor | 40 kW (servo motor) |
| Production Speed | 30 m/min |
| Transmission | Gear / sprocket drive, 1.5-inch chain |
| Cutting Tolerance | ±1 mm |
| Machine Dimensions | 12,400 × 2,000 × 2,100 mm |
| Machine Weight | Approx. 20.2 T |
Standard configuration: 5-ton manual decoiler, hydraulic front shear, 7-roller leveling, hydraulic pre-punching station (flange + bottom holes), hydraulic post-cutting, Siemens PLC control, Omron encoder, wireless remote controller.
Inspection standard: 2.0 mm thickness galvanized steel. Custom thickness and yield strength configurations are available on request.
Frame Options: Pillar-Type vs Archway-Type
| Feature | Pillar-Type | Archway-Type |
| Side Plate | 59×59 mm | 38 mm |
| Machine Weight | Approx. 17.4 T (Z100-300) | Approx. 15 T (Z100-300) |
| Forming Stations | 16 + 1 + 1 | 15 + 1 + 1 |
| Main Drive Motor | 30 kW | 30 kW |
| Best For | Heavy-duty, high-rigidity production | Standard production, space-saving |
| Web Height Range | 45–80 mm | 45–80 mm |
Both frame types use the same Cr12 rollers, Φ75 mm shafts and 450H frame specification. The pillar-type offers higher rigidity for thick high-strength steel, while the archway-type provides a more compact footprint.
Punching & Cutting Configuration
Pre-punching stations: 3 punching units for bottom double holes, bottom single hole and side flange double holes
Standard hole size: 14×22 mm
Punch cylinder bore: Φ110 mm
Front shear: Cr12MoV flat-plate shear, design eliminates falling slugs, suitable for sheets ≥2.5 m. Single cylinder bore: Φ140 mm (Z100-300 archway-type and pillar-type) / Φ160 mm (Z100-350)
Back shear: Universal shear with Cr12MoV heat-treated blades
Cutting tolerance: ±1 mm
Tooling material: Cr12MoV tool steel, heat-treated for extended wear life
Decoiler Options
| Option | Specification |
| 5-ton Cantilever Decoiler (650 mm) | 5T capacity, unpowered, mechanical passive type. Coil ID: 508 mm, max coil OD: 1,500 mm, mandrel expansion: 450–520 mm, coil width: 650 mm |
| 5-ton Hydraulic Expansion Decoiler (650 mm) | 5T capacity, hydraulic expansion, pump power: 3 kW, inverter speed control, motor power: 3 kW, dual support rods. Coil ID: 508/610 mm, max coil OD: 1,600 mm, mandrel expansion: 460–530 mm and 560–630 mm, coil width: 650 mm |
Core Components & Build Quality
All our Z purlin roll forming machine lines are built with industrial-grade components for reliable long-term operation:
1. Decoiler
Manual cantilever or hydraulic expansion options, with 5-ton load capacity and compatibility with standard steel coil inner diameters.
2. Pre-Leveling Unit
7-roller leveling unit (4-over-3 arrangement) with Φ95 mm leveling rollers removes coil set and ensures flat, consistent strip feeding. Width adjustment scales accommodate variable coil widths.
3. Hydraulic Punching System
Multi-station pre-punching with three independent punching units delivers accurate hole positioning. All punch and die tooling is manufactured from Cr12 tool steel with heat treatment. Punch cylinder bore: Φ110 mm.
4. Forming Main Frame
Heavy wall-plate welded structure with 450H frame for low-vibration operation. Forming rollers are made from Cr12 tool steel (hardness equivalent to D3) , heat-treated, hard chrome plated and precision machined to mirror finish. Shafts are Φ75 mm, 45# steel, precision machined.
5. Hydraulic Cutting System
Post-forming universal shear with Cr12MoV tool steel blades for clean, burr-free cuts. Front shear uses Cr12MoV flat-plate blades with design eliminates falling slugs. Slug breakers are included for high-volume production.
6. PLC Control System
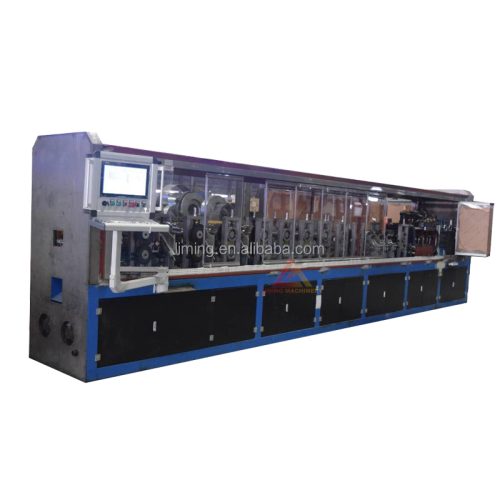
Siemens PLC with touchscreen HMI, Omron encoder and wireless remote controller for automatic length control, batch counting, punching quantity and parameter setting. Integrated control cabinet manages web width and flange height changeover.
Key Benefits of Z Purlin Roll Forming Machines
Investing in a purpose-built Z purlin machine delivers measurable operational and financial benefits:
1. Superior Structural Performance
Z purlin overlapping flange design enables continuous load transfer across spans, making it ideal for large industrial roof systems.
2. High Production Efficiency
Continuous coil-fed operation delivers consistent high-volume output at 30 m/min, significantly faster than press-brake or piece-by-piece forming.
3. Precise Dimensional Accuracy
Progressive forming, Cr12 rollers and closed-loop PLC control ensure uniform profile dimensions and repeatable hole positioning across every batch. Cutting tolerance reaches ±1 mm.
4. Flexible Production Options
Choose from pillar-type or archway-type frames, and from Z100-300 or Z100-350 models to match your profile range and production volume.
5. Low Material Waste
Continuous roll forming achieves material utilization rates above 95%, with pre-shearing only trimming irregular coil heads and tails.
6. Reduced Labor Dependency
Automated feeding, punching, forming and cutting minimize manual intervention. One operator can manage the entire line with the wireless remote controller.
Price Factors & ROI
The price of a Z purlin roll forming machine depends on several configuration factors:
Maximum web height and material thickness capacity
Number of forming stations
Punching configuration (3 units standard)
PLC brand and automation level
Decoiler type (cantilever vs hydraulic expansion)
Custom engineering requirements
Shipping and on-site installation
A compact line costs significantly less than a fully-automatic line equipped with hydraulic-expansion decoiler and complete auxiliary functions. To evaluate ROI, calculate:
Daily production output at 30 m/min
Labor cost reduction (one operator per line)
Material utilization rate above 95%
Energy consumption
Annual maintenance cost
Expected machine service life
For a tailored quotation based on your profile drawing, contact our sales team.
How to Choose the Right Z Purlin Machine
Selecting the right Z purlin forming machine depends on your production volume, project variety and operational requirements. Consider these key factors:
1. Profile Size Range
If your projects require web heights up to 80 mm, choose the Z100-300 model. For web heights up to 100 mm, choose the Z100-350 model.
2. Frame Type
Choose pillar-type for heavy-duty production requiring maximum rigidity. Choose archway-type for standard production with a more compact footprint.
3. Material Thickness & Strength
Standard models process 1.5–3.0 mm steel with yield strength of 235 MPa or 345 MPa. For thicker or higher-strength steel, custom configurations are available.
4. Punching Requirements
Define your hole patterns, sizes and positions. Our standard configuration includes three punching units for bottom double holes, bottom single hole and side flange double holes at 14×22 mm. Custom hole patterns can be engineered.
5. Production Speed & Volume
Our automatic models run at 30 m/min, suitable for high-volume production. The 40 kW servo motor on the Z100-350 delivers higher torque for thicker material.
6. Automation Level
Standard configuration includes Siemens PLC, Omron encoder and wireless remote controller. Hydraulic expansion decoiler is available for higher automation.
If your projects require both C and Z profiles, a CZ purlin roll forming machine can handle both. The CZ purlin machine switches between C and Z profiles automatically. Learn more in our automatic C/Z purlin roll forming machine guide.
To evaluate suppliers before ordering, read our how to choose CZ purlin manufacturer guide.
For projects that also need C/U profiles, see our C/U purlin roll forming machine.
Not sure which Z purlin configuration matches your production needs? Contact our engineering team for a free configuration recommendation.
Basic Maintenance Tips
Regular maintenance extends machine service life and maintains profile accuracy:
Lubricate bearings and moving parts according to the manufacturer's schedule
Clean forming rollers and guide surfaces daily to prevent surface scratches
Inspect punching dies and Cr12MoV shear blades regularly; replace or sharpen when worn
Check hydraulic oil level and replace filters on time
Back up PLC programs and parameter settings periodically
For detailed maintenance procedures or troubleshooting, contact our technical support.
Frequently Asked Questions
Q1: What is the difference between a Z purlin machine and a C purlin machine?
A C purlin roll forming machine produces symmetrical C-shaped profiles for wall framing and single-span roofs. A Z purlin machine produces offset Z-shaped profiles with overlapping flanges for continuous load transfer across long roof spans. For a detailed comparison, read our full C purlin roll forming machine guide.
Q2: Can one Z purlin roll forming machine produce different sizes?
Our automatic Z purlin machines can adjust web height and flange width via the integrated control cabinet. The Z100-300 covers web heights of 45–80 mm, and the Z100-350 covers 45–100 mm. Custom sizes are available on request.
Q3: What thickness can a Z purlin forming machine process?
Standard Z purlin forming machine models process 1.5–3.0 mm thick steel, with yield strength of 235 MPa or 345 MPa. 2.0 mm galvanized steel is the standard inspection thickness.
Q4: What is the cutting accuracy of a typical purlin roll forming machine?
Our standard Z purlin machines achieve ±1 mm cutting length tolerance using Cr12MoV universal shear blades and Omron encoder control.
Q5: What is the typical delivery time for a Z purlin roll forming machine?
Standard production lead time is 80 working days from receipt of advance payment. Machines are packaged for shipment in a single 40GP container.
Q6: What after-sales support is included with a Z purlin machine?
We provide 12-month warranty on core components, overseas on-site installation guidance, operator training and lifetime technical consultation. Spare tooling kits are included with all punching configurations.
Related Reading
C purlin roll forming machine guide
Automatic C/Z purlin roll forming machine complete guide
How to choose CZ purlin manufacturer
C/U purlin roll forming machine
Solar mounting roll forming machine
Looking for a Reliable Z Purlin Roll Forming Machine?
Xiamen Zheng Liming supplies automatic Z purlin production lines in both pillar-type and archway-type frames for steel fabricators, prefab builders and construction material suppliers worldwide. Every line is engineered to match your exact profile drawing, material requirements and production capacity.
✅ Free technical drawing evaluation
✅ Factory-direct FOB Xiamen pricing
✅ Overseas installation & operator training
✅ 12-month warranty on core components